Adjustable tap wrench
 Countersink bit set
 Countersink Bits
 Limit Plug Gauges
 Machine tab
 Machine Tap + Twist Drill
 Metal drill bit
 Metal drill bit sets
 Round die sets
 Round dies
 Screw Pitch Gauges
 STI HexTap V-COIL
 Tab and Drill set
 Tang break tool
 Tap and die sets
 Tap Holder with Ratchet
 Thread cutting oil
 Thread plug gauge
 Thread tap
 Threading bit set
 Threading repair sets
 V-coil
 V-COIL Inserting tool
 VÖLKEL Running Shirt
 Wood drill bit
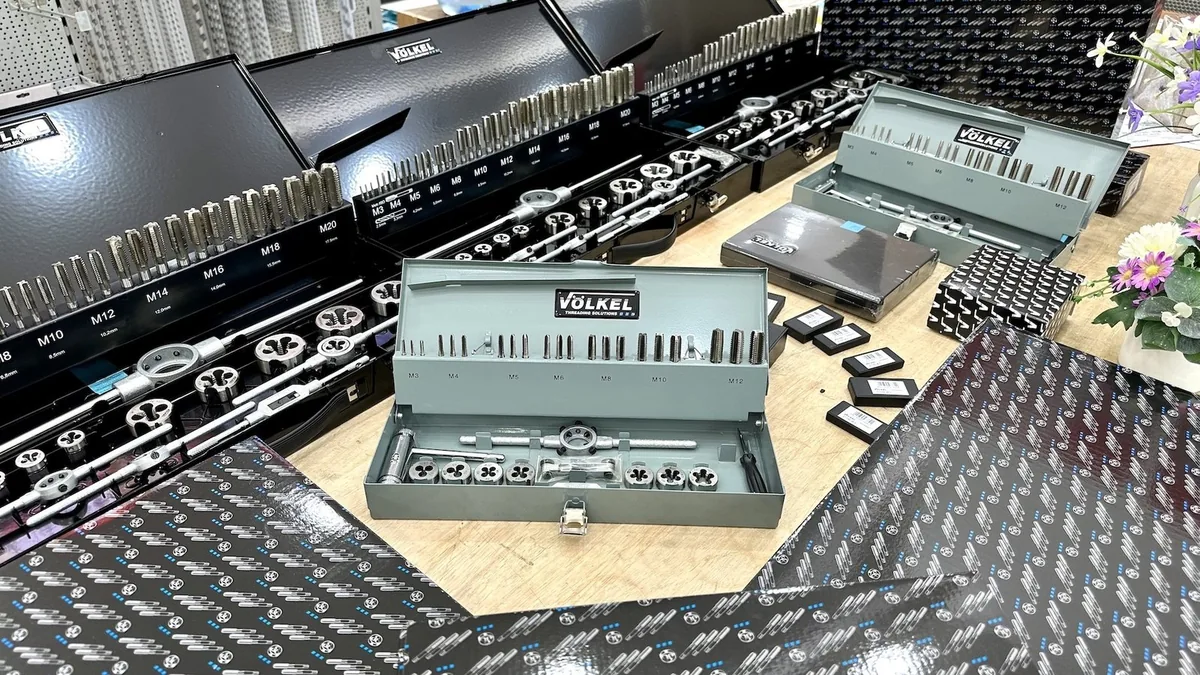
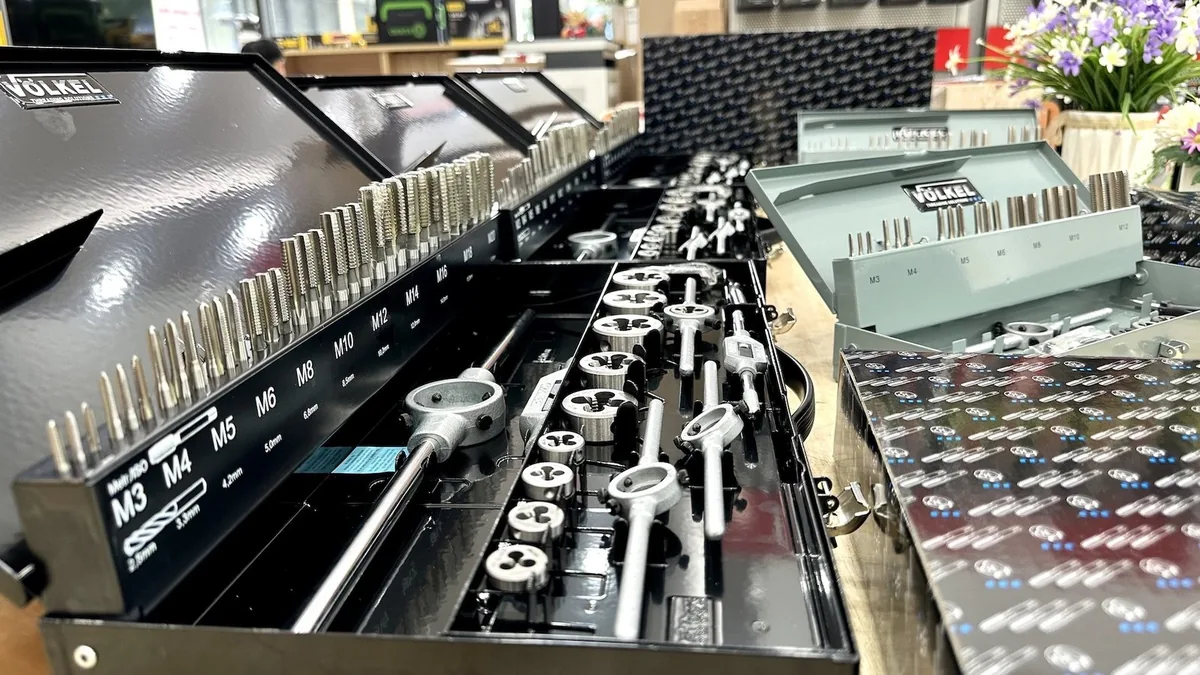
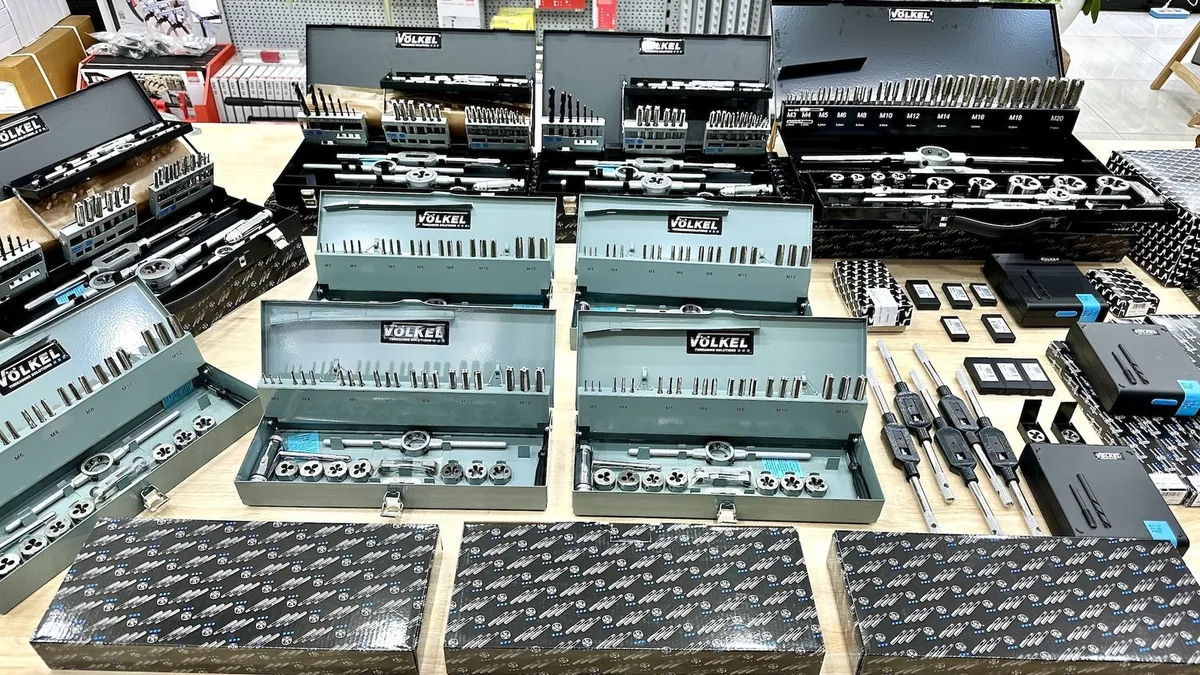
Tap and die sets are used to form internal and external threads in metal, in machine shops as well as in equipment maintenance and repair work. This group covers HSS-G or HSS-E hand taps for cutting internal threads in holes, and thread cutting dies for cutting external threads on shafts and bolts. The size range runs from M3 to M30 in the ISO metric system, covering common requirements in Vietnam and Europe.
Dedicated sets also cover Whitworth BSW threads and unified UNC and UNF threads. BSP pipe threads serve piping and sanitary equipment installation. The piece count ranges from 22 to 62 pieces depending on the size range and the tap configuration. Some sets include drill bits for preparing the hole, making the threading sequence more continuous.
Voelkel.vn is the authorised VÖLKEL distributor in Vietnam, with confirmed German origin and warranty according to the manufacturer's standard.


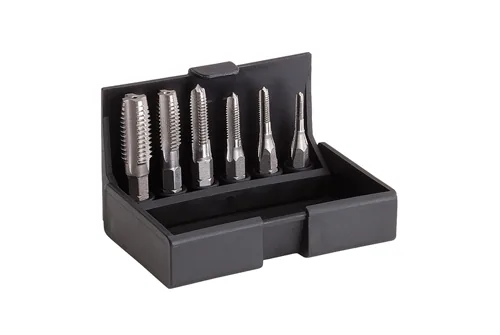
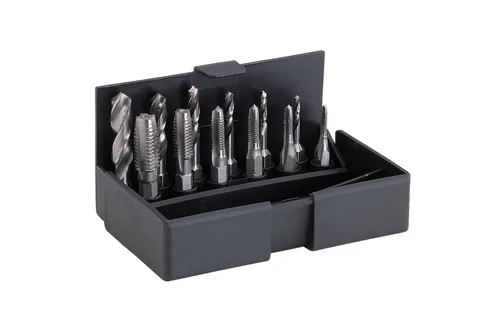
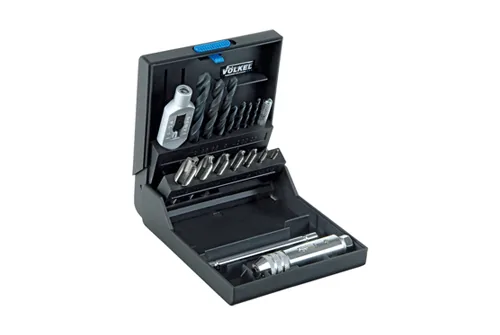

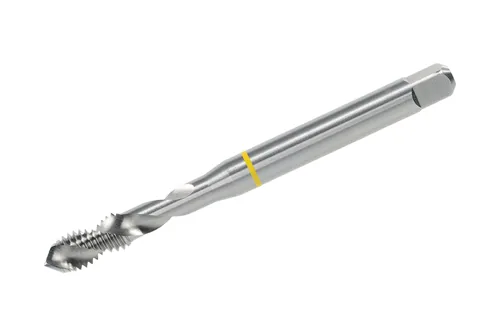

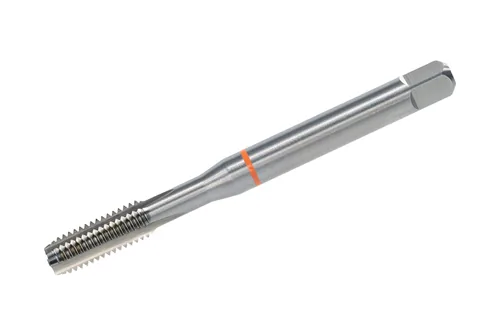
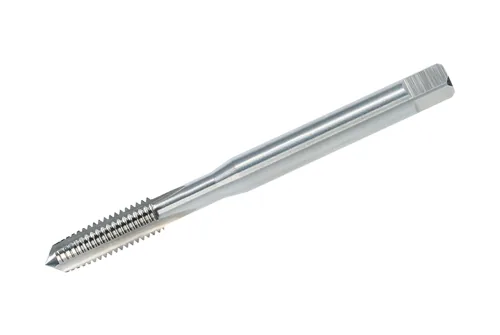
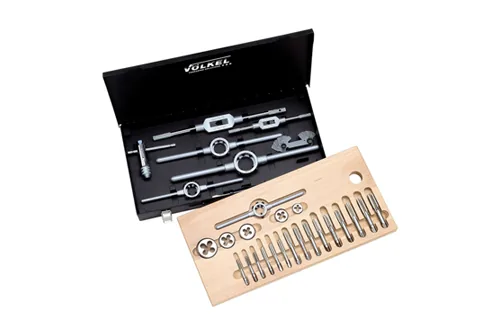
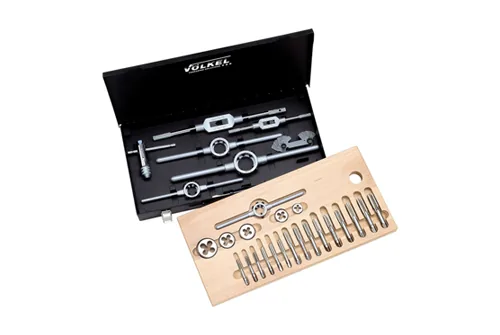
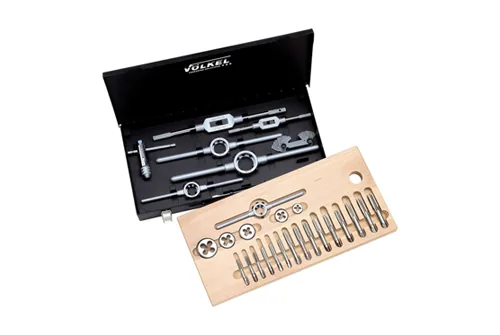

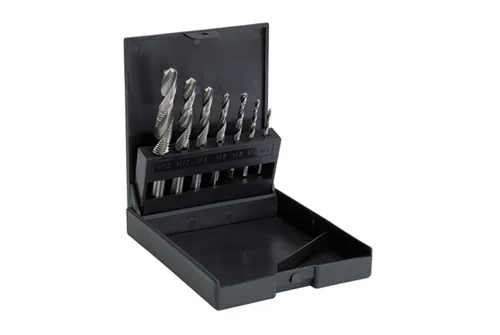
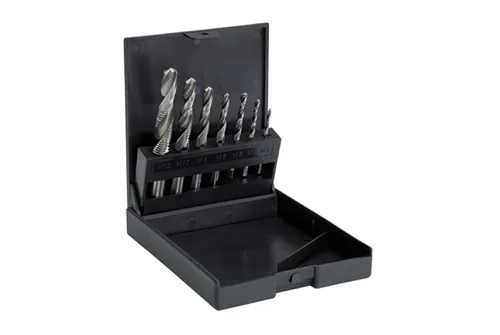
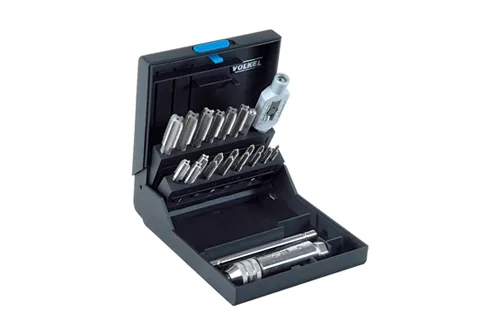

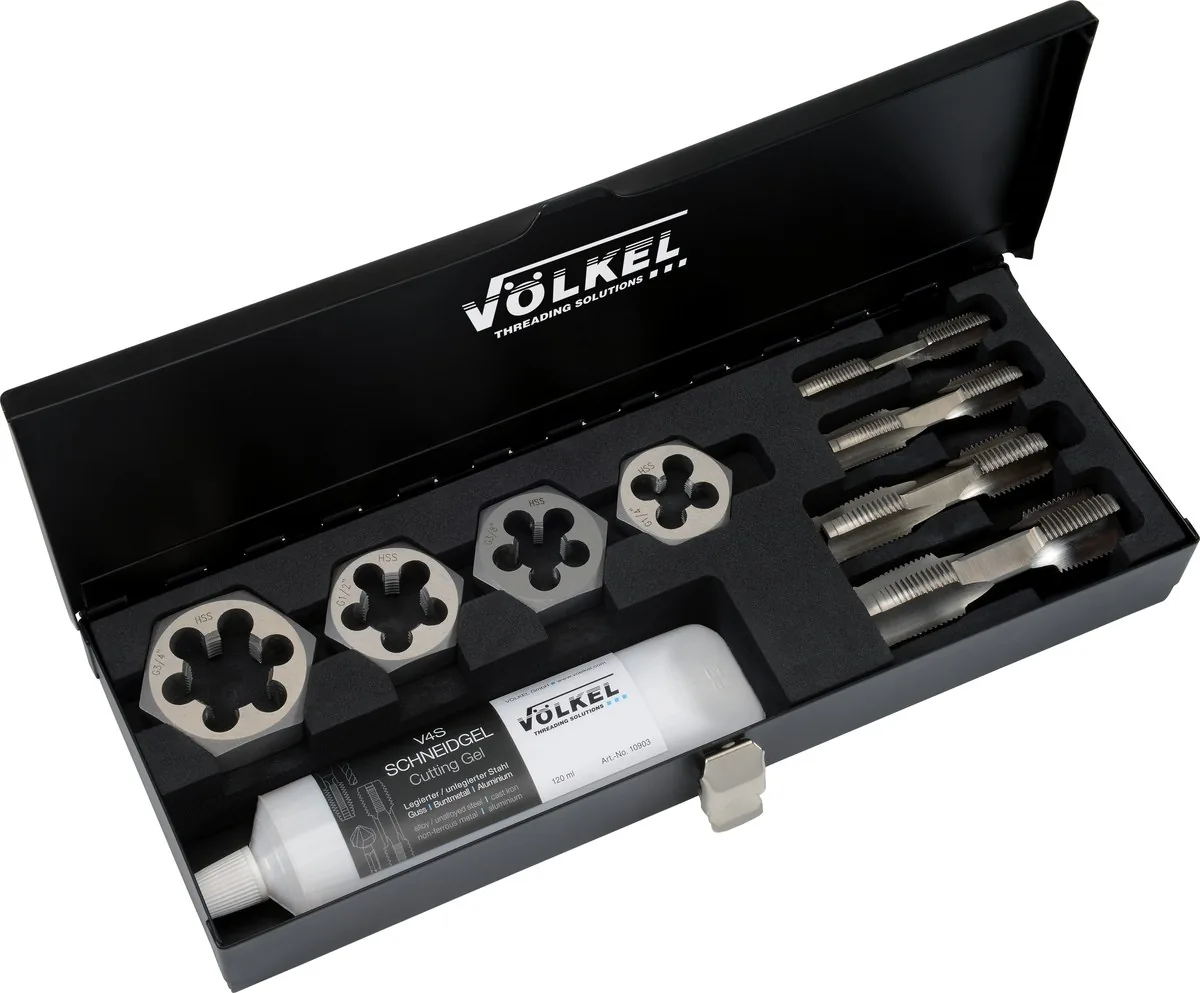

Tab and round die sets are used to produce internal and external threads on metal, in machine shops, maintenance departments and equipment repair. This product group includes HSS-G or HSS-E hand taps for cutting internal threads in holes, and external round dies for cutting threads on shafts and bolts. The size range runs from M3 to M30 in the ISO metric system, covering common requirements in Vietnam and Europe.
Dedicated sets also cover the Whitworth BSW system, Unified UNC and UNF threads. BSP pipe threads serve pipework and sanitary installation. The number of pieces ranges from 22 to 62 depending on the size range and the tap configuration. Some sets come with drill bits for hole preparation, making the threading workflow more continuous.
Voelkel.vn is the authorised VÖLKEL distributor in Vietnam, with German origin confirmed and warranty according to the manufacturer's standard.
Tab and round die sets are used to cut internal threads in holes and external threads on shafts or bolts. Hand taps cut the thread inside the workpiece, while external round dies cut the thread on round stock. This pairing lets machine shops, maintenance and repair teams handle threading work on their own. The ISO metric size range across the group runs from M3 to M30.
The cutting edge material is mainly HSS-G and HSS-E, which affects tool life and the ability to machine harder materials. Code 49101 uses HSS-G with 43 pieces from M3 to M12. Code 49251 uses HSS-E, with 52 pieces from M3 to M20, including a tap wrench and a die holder.
The thread system determines whether the tool and the workpiece to be machined will mate. Each system has its own flank angle, pitch and nominal diameter. Identifying the thread system correctly before cutting helps avoid damaging the workpiece. This product group covers ISO metric threads, Whitworth BSW, Unified UNC and UNF threads, together with BSP pipe threads.
The ISO metric system accounts for most configurations in the group. Code 49107 has 35 pieces for the M3 to M12 range. Code 49201 has 54 pieces for the M3 to M20 range, with three taps per size — taper, second and bottoming — plus one external round die.
The inch thread group serves parts made to British and American standards. Code 48050 has 27 pieces in UNC from 1/4 to 1/2. Code 48051 extends the UNC range to 1/4 through 3/4 with 35 pieces. UNF threads are covered by code 48060 with 22 pieces from 1/4 to 1/2.
Whitworth BSW threads appear in code 48030, with 36 pieces for the 1/8 to 1/2 range. BSP pipe threads serve pipework and sanitary installation. Code 48650 contains taps and hexagon die nuts for the G 1/4 to 3/4 range. The corresponding HexTap version carries code 48651.
The piece count per set ranges from 22 to 62. The figure depends on the size range and the tap configuration included. Smaller sets focus on common thread sizes, while larger sets span a wider diameter range. Some configurations also include drills for hole preparation, shortening the step between drilling and tapping.
The M3 to M12 range suits assembly work and repair of small parts. Code 49114 uses HSS-G for this range. Code 49151 has 43 HSS-E pieces including drills. Code 49106 increases this to 50 pieces, also with drills for the same size range.
The M3 to M20 range additionally covers larger bolted joints. Code 49205 has 52 pieces for this range. When even larger diameters are needed, code 48006 extends to M24 with 61 pieces. Choosing a wider range reduces how often individual tools have to be added later.
Some mechanical joints require left-hand threads to prevent self-loosening caused by the direction of rotation. The group includes left-hand configurations marked LH alongside the usual right-hand versions. There are also taper configurations, that is, taps with a long chamfered lead for easier thread entry. Read the designation carefully before ordering to avoid mixing up the thread direction.
Code 49171 has 43 left-hand pieces from M3 LH to M12 LH, including drills. Code 49271 extends left-hand threads to the M3 LH to M20 LH range with 52 pieces. These two configurations cover the tooling that right-hand sets cannot handle.
The taper configuration carries code 49183 in HSS-G for the M3 to M12 range. Code 49181 has 43 pieces including drills for the same range. Code 49150 provides 50 pieces including drills, intended for shops that need tooling ready for repeated threading work.
Alongside the general-purpose sets, the group also contains configurations tied to a particular family of parts. These sets focus on recutting and cleaning damaged threads rather than producing new threads on blank stock. The piece count is usually smaller and the thread sizes are selected according to the actual work involved.
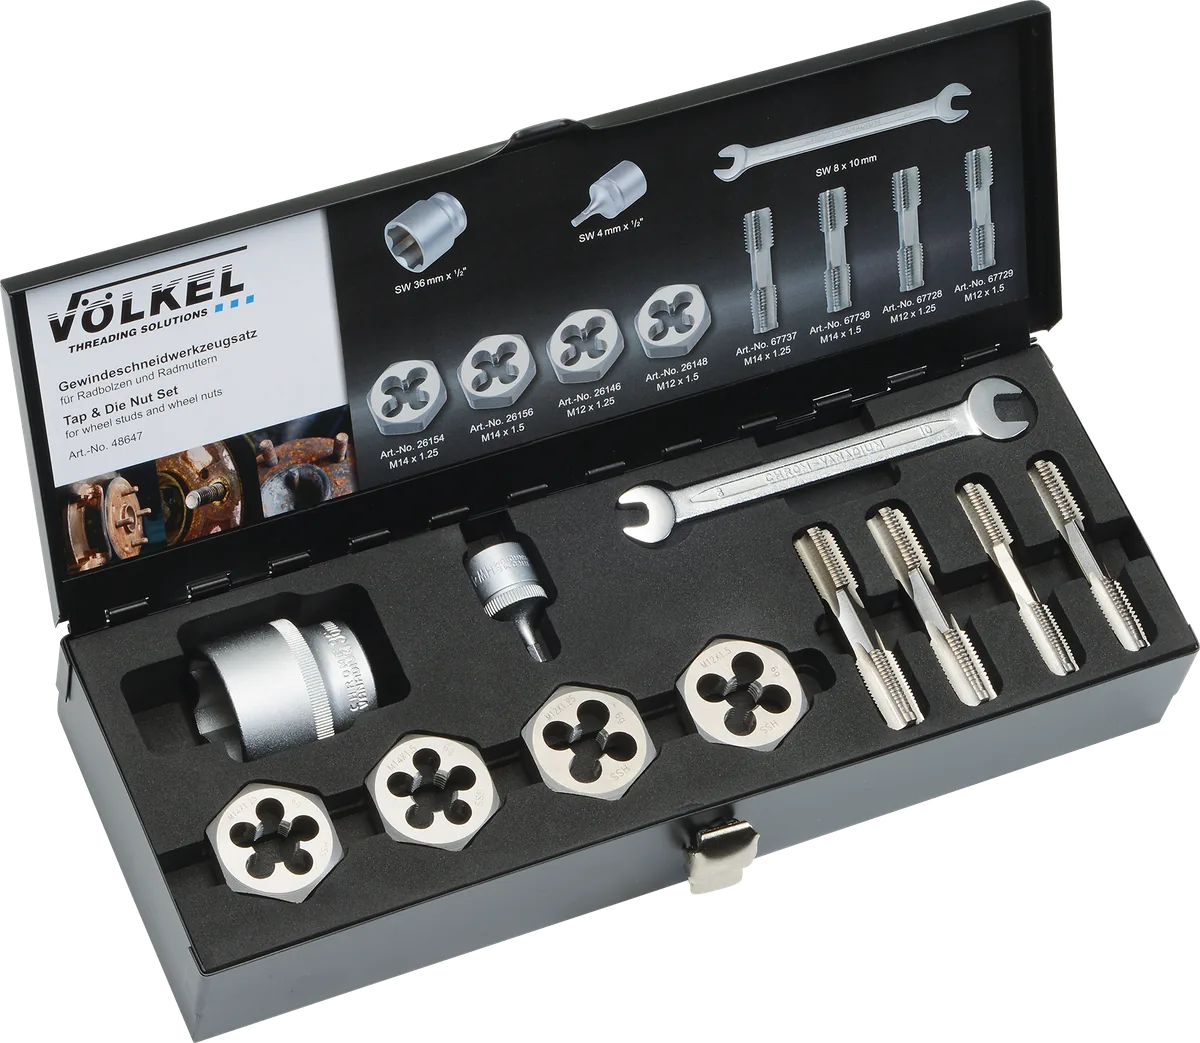
Code 48647 has 11 pieces for wheel studs and wheel nuts, for recutting damaged internal and external threads. Code 47008 is intended for grease nipples, small parts found on vehicles, construction machinery and agricultural machinery.
Code 22890 combines a short machine tap with an external round die for BSF 3/8 x 20 threads. The 111th anniversary edition carries code 99WM42, in HSS-G to DIN standard for the M3 to M12 ISO metric range.
Selection starts with the thread system you work with, then the diameter range used regularly. The workpiece material influences the choice between HSS-G and HSS-E. If the work also includes drilling pilot holes, a configuration with drills keeps the workflow continuous. Left-hand or right-hand direction should be determined from the outset.
Multi-task maintenance shops usually prefer a wide range and a high piece count. Operations focused on one family of parts can choose a dedicated repair set to reduce surplus tooling in stock. When cutting, align the die squarely from the first thread turn so the thread starts in the correct direction.
You can view the details of each code on the corresponding product page to compare piece count, size range and material before ordering.